Top Sanitary Mixer Design Features That Matter
A sanitary mixer is not made hygienic by a polished exterior or a stainless-steel nameplate. Its real performance is determined at the product-contact surfaces, shaft penetrations, discharge valve, and the areas operators must access between batches. The top sanitary mixer design features directly affect cleanout time, cross-contamination risk, batch repeatability, and the labor required to keep a process ready for production.
For food, pharmaceutical, cosmetic, and specialty chemical manufacturers, the right specification begins with the material and cleaning method, not a generic equipment checklist. A ribbon mixer handling free-flowing seasoning blends has different sanitary demands than a unit processing cohesive nutraceutical powders, wet granulations, or high-viscosity pastes. The objective is the same: deliver homogeneous mixing while making every product-contact area practical to inspect, clean, validate, and maintain.
Top Sanitary Mixer Design Features to Specify
Product-contact materials and surface finish
Type 304 or 316 stainless steel is the starting point for many sanitary mixer applications, but material selection should match the product, wash chemicals, temperature, and corrosion exposure. Type 316 stainless steel is often selected where chlorides, acidic ingredients, aggressive cleaning agents, or elevated corrosion resistance are concerns. It is not automatically necessary for every application, and selecting a higher-grade alloy without reviewing the full process can add cost without solving the real sanitation issue.
Surface finish matters just as much. A smooth, consistent product-contact finish reduces locations where powders, oils, binders, and fine particles can adhere. The required roughness level depends on the industry, product characteristics, and internal sanitation standard. Pharmaceutical and high-purity applications may require tighter finish specifications and documented inspection, while some dry bulk applications can achieve dependable cleaning with a less demanding finish. What matters is that the finish is specified across the trough, ribbon assembly, shaft areas, end plates, and discharge components – not only on visible external panels.
Continuous welds with a clean, accessible profile
Weld quality is a process requirement. Crevices, pits, undercuts, and irregular weld profiles can retain material and complicate washdown or dry cleaning. Product-contact welds should be continuous, properly finished, and accessible for visual inspection where possible.
The detail is especially relevant in ribbon mixers because the agitator contains multiple attachment points. Ribbon-to-arm connections, support members, and shaft interfaces must be engineered to prevent product accumulation without compromising mechanical strength. A design that is easy to fabricate but difficult to clean will create recurring downtime throughout its service life.
Hygienic shaft seals and bearing placement
The agitator shaft is one of the most critical sanitary design areas. Seals must control product leakage and prevent outside contaminants from entering the mixing zone, while tolerating the mixer’s operating conditions. Fine powders, sticky products, vacuum operation, pressure differentials, and washdown exposure can each change the appropriate seal design.
External bearing placement is generally preferred for sanitary processing because it keeps lubricants and bearing wear outside the product zone. The shaft penetration should be designed for access and cleaning, with a seal arrangement suited to the material. For demanding applications, options may include air-purged seals, specialized mechanical seals, or configurations designed for vacuum service. The correct answer depends on the product and operating cycle; a seal that works well for dry food ingredients may not be suitable for a paste with aggressive cleaning requirements.
Full-access covers and inspection points
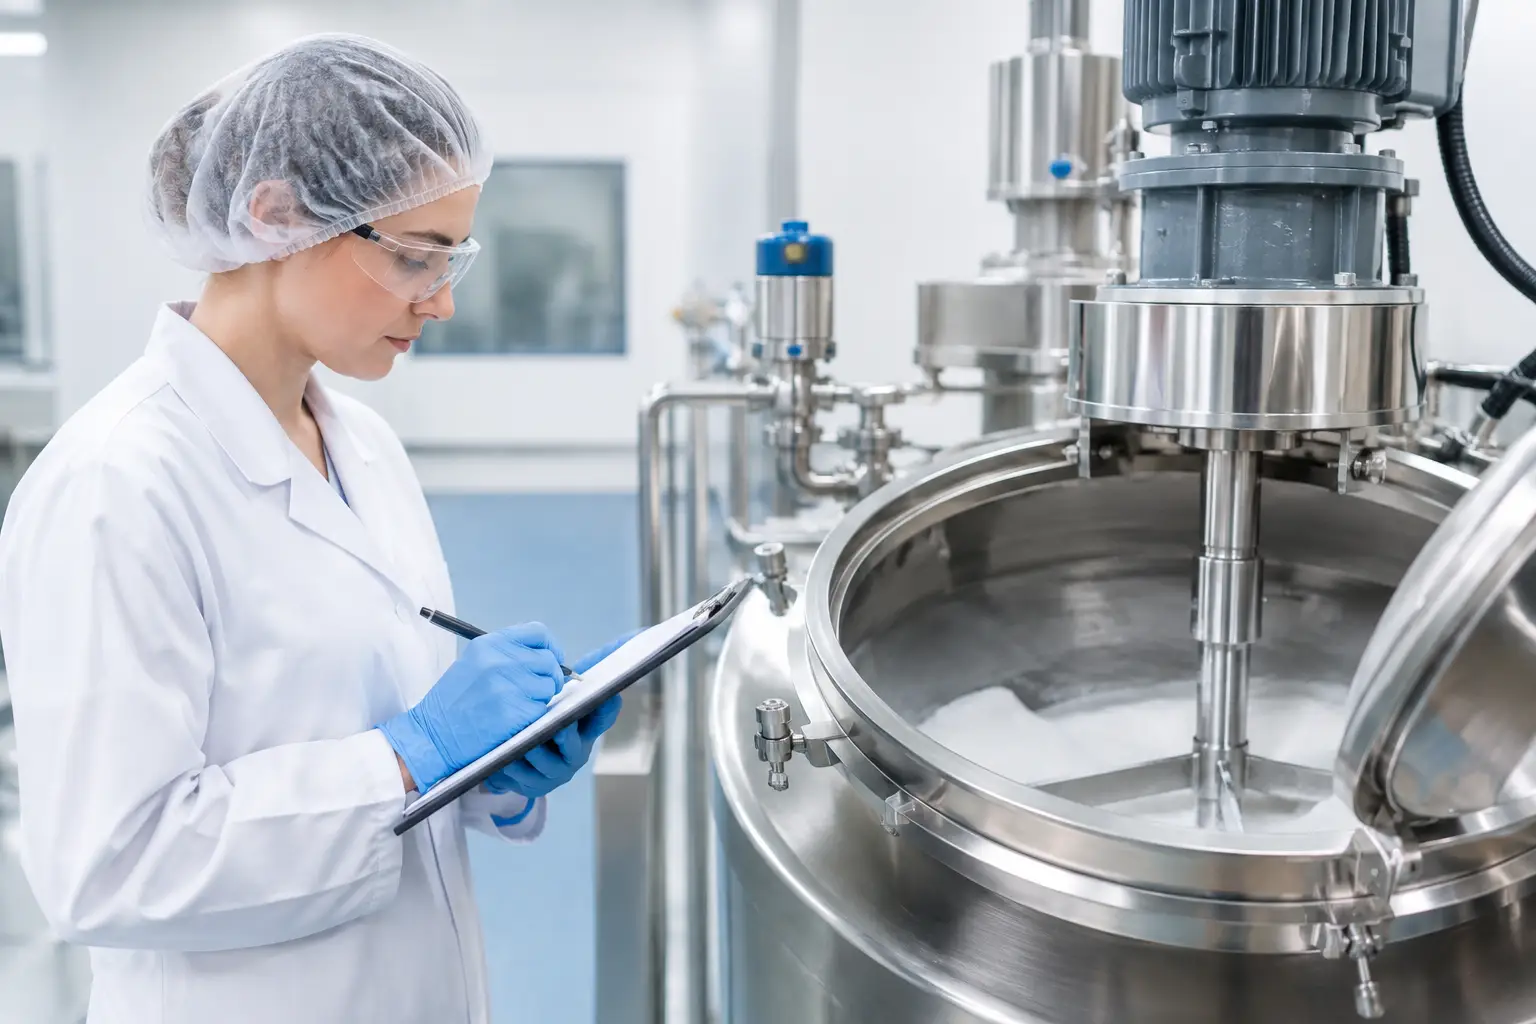
A sanitary mixer must be cleanable in the real conditions of a production floor, not just in a design review. Large, properly located access covers allow operators to inspect the trough, ribbons, end zones, and discharge area. Covers should open safely, provide adequate clearance, and use hygienic gaskets that do not create unnecessary retention areas.
For manual cleaning or product changeovers, full-access openings can reduce the time spent reaching around internal components. For validated cleaning programs, access also makes it easier to perform swab testing and visual verification. Small inspection ports have value, but they do not replace access that allows a technician to assess the entire product-contact interior.
A discharge valve designed for complete emptying
Many sanitary challenges appear at discharge. A mixer may blend well, yet leave product behind in a poorly designed valve, outlet transition, or dead area beneath the trough. Residual material can affect yield, create allergen or ingredient carryover, and delay changeovers.
The discharge valve should match the product’s flow behavior. Free-flowing powders may discharge efficiently through a flush-mounted valve, while cohesive powders, damp mixtures, or pastes may require a different geometry or a larger outlet. The best design minimizes product hold-up and supports controlled discharge without compromising batch integrity. Valve actuation, seals, and cleanout access should all be considered early, especially when the mixer feeds downstream packaging, conveying, or granulation equipment.
Clean-in-place or wash-in-place capability where justified
CIP or wash-in-place systems can improve sanitation consistency and reduce manual labor, but they are not automatically the best choice for every ribbon mixer. Dry powder operations often use dry cleaning, vacuum removal, or controlled wipe-down procedures to avoid introducing moisture that can cause caking or microbial concerns. In contrast, wet, sticky, allergen-sensitive, or high-care applications may benefit from engineered spray devices and a defined wash cycle.
A successful CIP design requires more than adding spray balls. Coverage, fluid velocity, drainage, spray-device location, internal geometry, cleaning chemistry, and verification all need to work together. The ribbon assembly must not shield areas from cleaning action, and the mixer must drain effectively after washing. If a process requires CIP, the equipment should be designed around it from the beginning rather than modified after installation.
Sanitary Design Must Still Deliver Mixing Performance
Sanitary construction cannot be separated from mixer performance. Ribbon geometry, agitator speed, fill level, and batch cycle determine whether ingredients distribute uniformly without damaging fragile particles or creating segregation. Overemphasizing cleanability while overlooking the material’s mixing behavior can result in an attractive machine that does not meet blend uniformity targets.
Horizontal ribbon mixers are often effective for powders, granules, and pastes because the inner and outer ribbons generate a controlled counter-current movement through the batch. Their suitability, however, depends on bulk density, particle size distribution, cohesiveness, moisture level, and formulation. A low-fill or high-fill operating range, for example, may influence trough geometry and agitator selection. The sanitary specification should be developed alongside the mixing trial or process review.
Vacuum-capable ribbon mixer and dryer configurations introduce additional considerations. Vacuum-rated seals, vessel integrity, heating surfaces, and condensate management must coexist with cleanable product-contact construction. These systems can consolidate processing steps, but their specification requires a detailed understanding of the drying profile, solvent or moisture load, and cleaning procedure.
The Engineering Details That Reduce Downtime
The strongest sanitary designs reduce the number of compromises operators face during routine work. This includes hygienic gaskets that are easy to inspect and replace, safety interlocks that support safe cover access, and drive arrangements that permit maintenance without opening the product zone. External surfaces also deserve attention in washdown environments, where sloped ledges, sealed enclosures, and accessible frames can reduce water retention and cleanup effort.
Documentation is another practical feature, particularly in regulated production. Material certificates, weld records, surface-finish verification, operating instructions, and cleaning recommendations support qualification and internal quality programs. The level of documentation should fit the application. A pharmaceutical facility may require extensive turnover documentation, while a food ingredient producer may focus on material traceability, cleanability, and dependable service access.
Selecting a Sanitary Ribbon Mixer for the Actual Process
Before finalizing a mixer configuration, define the product’s flow behavior, batch size range, required blend uniformity, cleaning method, allergen or contamination controls, operating environment, and downstream discharge needs. It is also useful to identify how often formulas change and who will clean the equipment. A mixer cleaned once a month under controlled conditions can use a different access strategy than a unit changed over several times per shift.
PerMix approaches sanitary ribbon mixer selection as an application-specific engineering decision. Configurable troughs, agitators, covers, discharge arrangements, vacuum capability, and material options allow the equipment to support both production performance and sanitation requirements. The most cost-effective design is rarely the one with every available feature. It is the one that gives your operators a repeatable cleaning process, your quality team confidence in the result, and your production line the throughput it needs.
A well-specified sanitary mixer becomes easier to trust batch after batch: it blends consistently, releases product cleanly, and gives the plant a practical path to inspection and maintenance. That is where sanitation stops being a compliance burden and becomes a measurable production advantage.