What Causes Batch Variability in Industrial Mixing?
A formula can be correct on paper and still produce inconsistent results on the production floor. When one batch meets specification and the next requires rework, the issue is rarely a single obvious failure. Understanding what causes batch variability requires looking at the entire process: incoming materials, charging sequence, mixer geometry, operating parameters, cleaning practices, and the way material moves after discharge.
For manufacturers of powders, granules, pastes, and other bulk solids, batch variation affects more than product appearance. It can create quality holds, failed assays, customer complaints, excess scrap, longer changeovers, and unnecessary energy use. A disciplined approach to mixing process control turns variability from a recurring production problem into a measurable engineering opportunity.
What Causes Batch Variability in Industrial Mixing?
Batch variability occurs when the composition, physical properties, or performance of a finished batch differs from the intended target or from previous batches made under the same nominal recipe. In a dry blend, this may appear as uneven distribution of an active ingredient, colorant, flavor, or trace additive. In a paste or wet mix, it may show up as inconsistent viscosity, moisture content, particle dispersion, or bulk density.
The most challenging cases are caused by several small variations acting together. A modest change in raw material moisture may not matter by itself. Combined with a different fill level, shortened mixing time, and a partially blocked discharge gate, however, it can produce a material result that falls outside specification.
This is why operators should avoid treating every inconsistent blend as a mixer problem. The mixer is central to process performance, but it operates within a system. Consistent batches depend on controlling the variables before, during, and after the mixing cycle.
Raw Material Variation Starts the Problem
No mixer can fully compensate for ingredients that arrive with widely changing physical properties. Even materials purchased to the same specification can vary between suppliers, lots, seasons, and storage conditions.
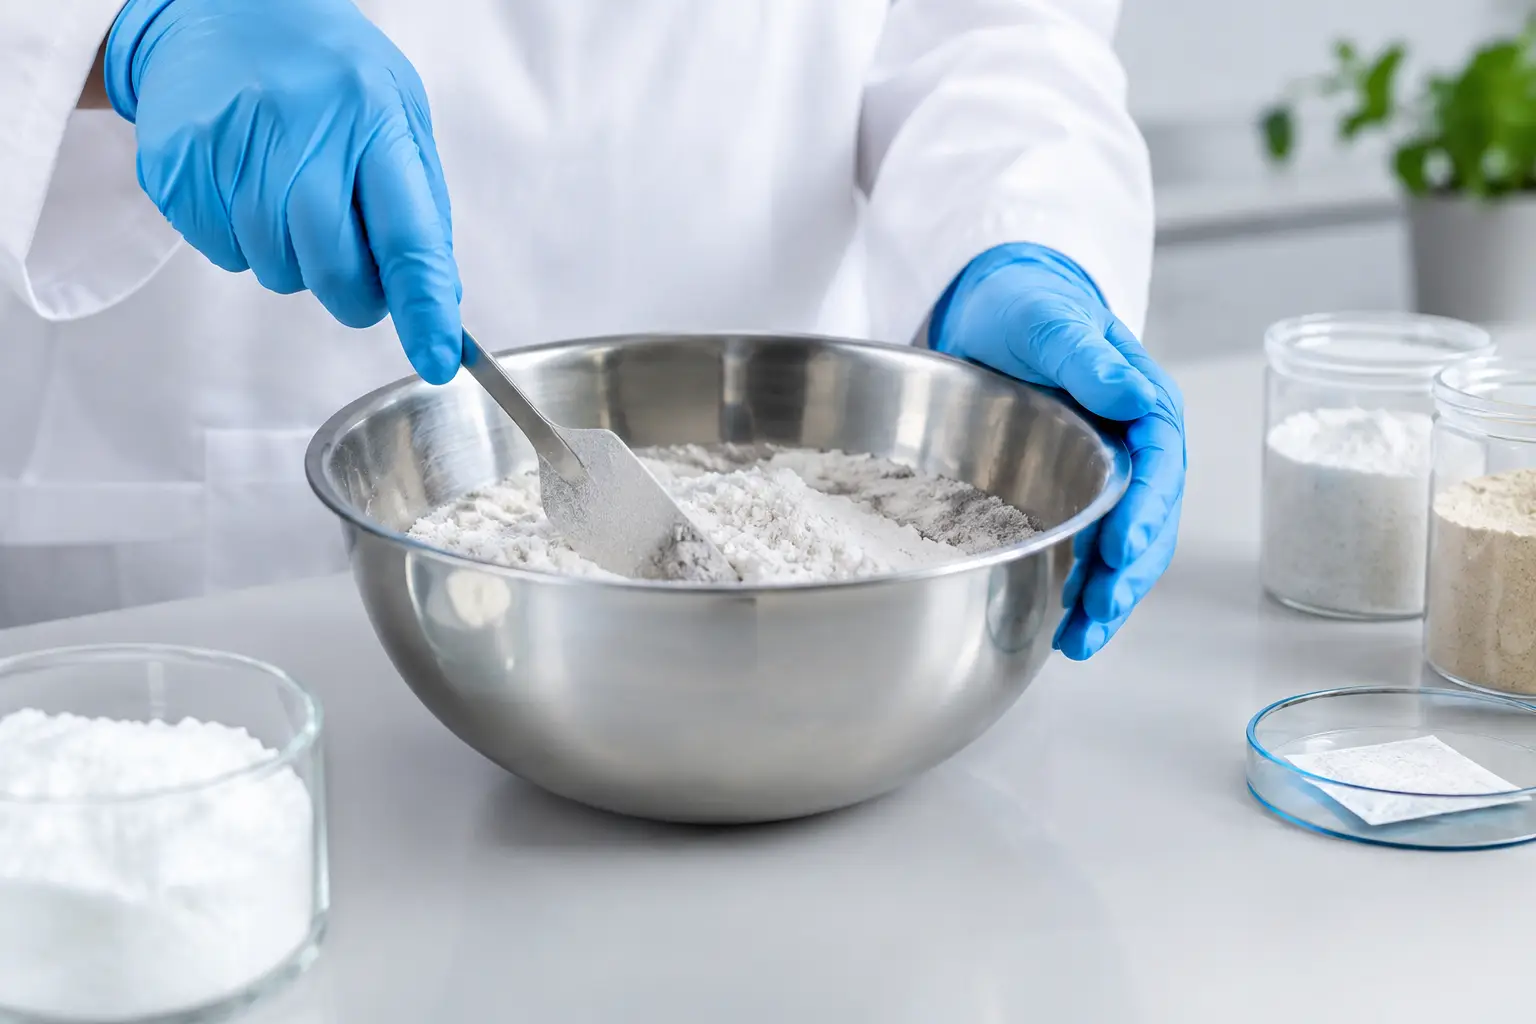
Particle size distribution is a common source of inconsistency. Fine particles tend to coat larger particles or form agglomerates, while coarse particles may separate during handling. When components differ substantially in size, shape, density, or flow behavior, they can segregate before they ever enter the mixer. A blend may look homogeneous at discharge but separate again during conveying, packaging, or transport.
Moisture is equally significant. Hygroscopic powders can absorb humidity during storage, changing their flowability and increasing their tendency to form lumps. Materials that are too dry may generate dust or electrostatic effects. Materials that are too wet may smear, bridge, or adhere to vessel walls and agitator surfaces. In food, chemical, agricultural, and pharmaceutical operations, controlling storage conditions and verifying incoming material moisture can prevent a large share of avoidable variation.
Bulk density changes also affect volumetric feeding. If a feeder is set by volume rather than mass, a lower-density ingredient can result in an undercharged batch even when the feeder appears to run correctly. For critical components, gravimetric dosing and documented lot verification provide much stronger control than relying on feeder settings alone.
Charging Errors and Ingredient Sequence Matter
The order in which ingredients enter the mixer has a direct effect on distribution. A minor ingredient added too early can collect in a dead zone or adhere to the vessel before the bulk material is present. Added too late, it may not receive enough mixing action to disperse uniformly.
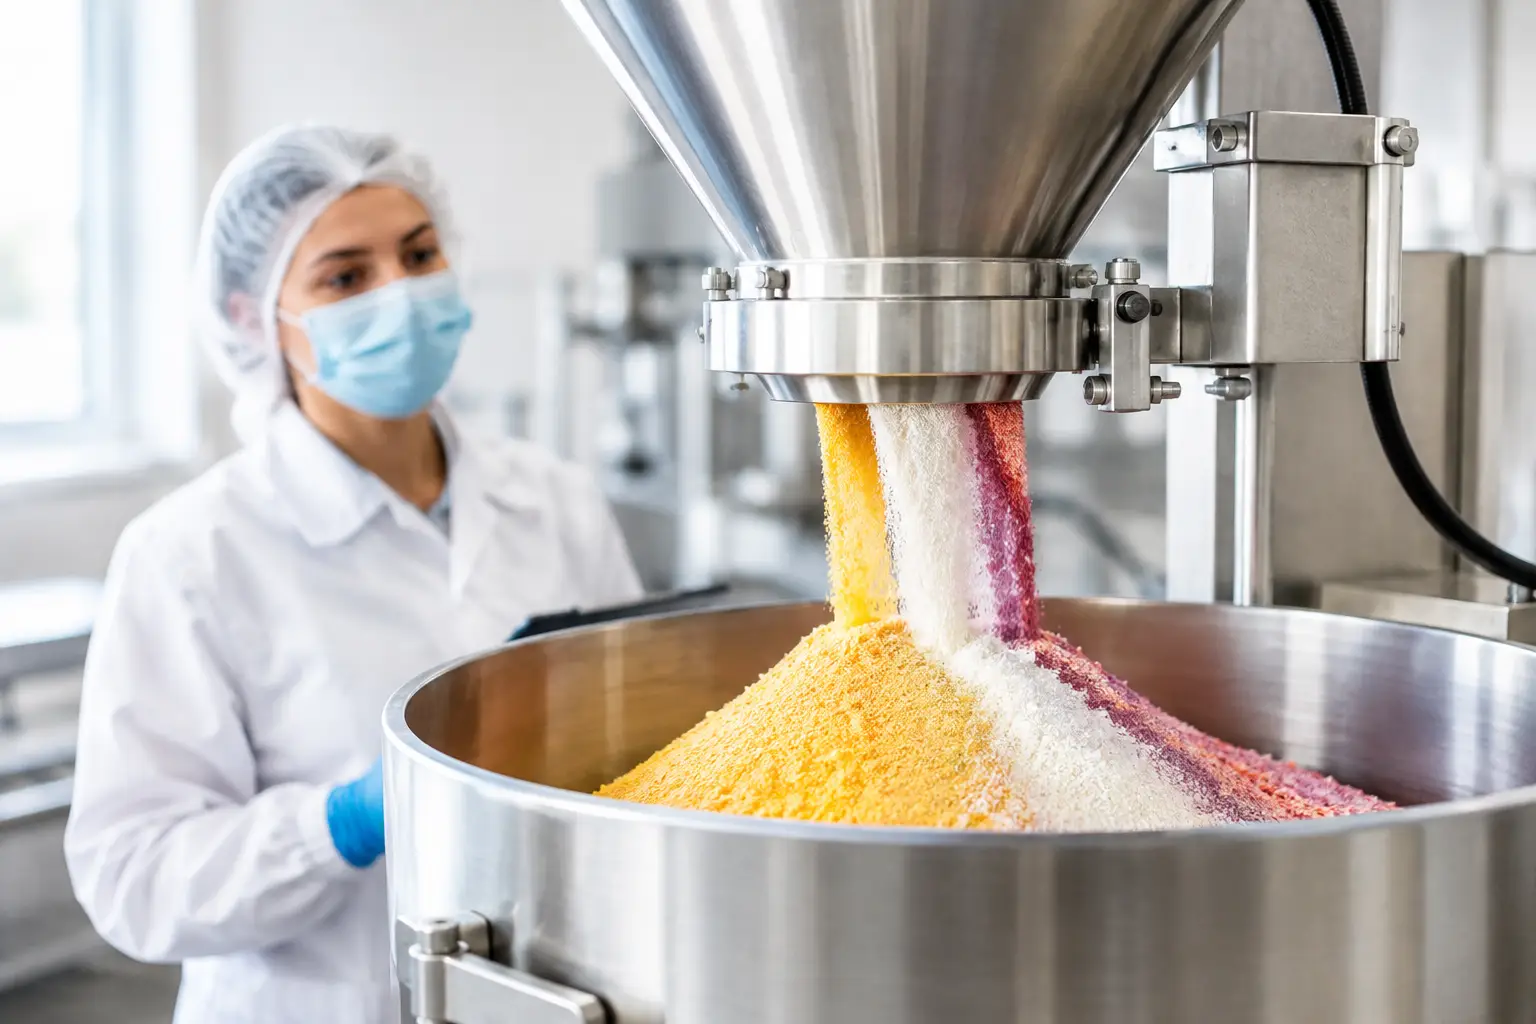
This is especially important for low-percentage additions. A colorant, vitamin premix, active pharmaceutical ingredient, lubricant, or liquid binder may represent only a small fraction of the total batch, yet it can determine whether the product passes or fails quality testing. These components often require a preblend, controlled addition point, or spray system rather than a simple top-entry dump.
Charging rate matters as well. Rapidly loading a ribbon mixer with poorly flowing powders can create compacted zones that take longer to break apart. Conversely, slow or intermittent feeding may allow early-added ingredients to migrate before the batch reaches its intended working volume. The goal is not merely to get material into the vessel. It is to create a repeatable starting condition for every cycle.
Mixer Fill Level and Operating Parameters
A horizontal ribbon mixer is designed to create a controlled pattern of axial and radial material movement. Inner and outer ribbons move material in opposing directions while lifting and folding the product through the vessel. That performance depends on operating within the mixer’s recommended working capacity.
Underfilling can reduce the material-to-agitator contact needed for efficient turnover. Overfilling limits the free movement needed for particles to circulate and redistribute. Both conditions can extend mixing time and increase the risk of uneven results. A mixer should be sized around the expected batch volume, material bulk density, and required operating range, not simply the largest theoretical vessel capacity.
Mixing time is another variable that is often misunderstood. Too little time produces incomplete distribution. Too much time can be just as problematic for blends with dissimilar particle characteristics because prolonged agitation may encourage segregation, particle attrition, heating, or damage to fragile ingredients. The correct endpoint should be established through representative sampling and validated against the actual material behavior.
Agitator speed, ribbon clearance, and shaft condition also influence repeatability. Changes in speed alter shear and circulation patterns. Worn ribbons or excessive clearance between the agitator and trough can leave material in low-movement areas. A process that once ran consistently may begin drifting as mechanical wear accumulates, even when the recipe and operator instructions have not changed.
Equipment Design Must Match the Material
Not every material behaves the same way in a standard ribbon mixer. Free-flowing powders, dense mineral blends, cohesive materials, fiber-containing products, and viscous pastes require different levels of agitation, clearance, discharge design, and optional features.
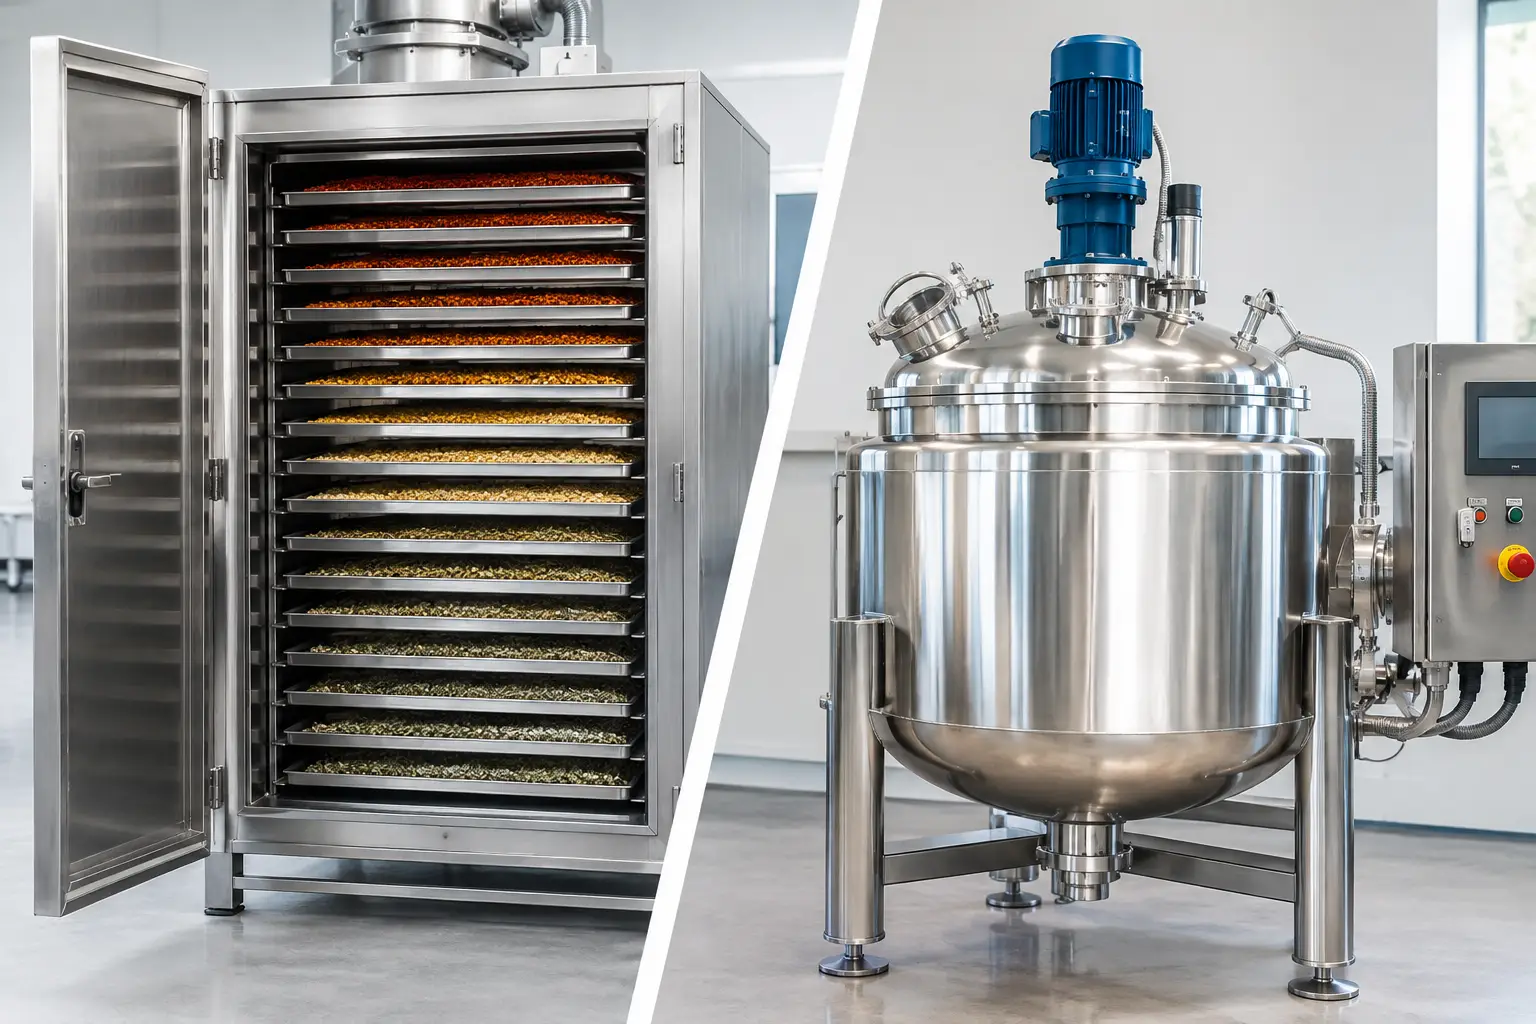
For example, highly cohesive powders may need a high-speed chopper to break agglomerates during the main mixing cycle. Liquid additions may require an atomizing spray bar to distribute a binder or oil across the moving product bed. Vacuum capability may be necessary where drying, deaeration, solvent removal, or temperature-sensitive processing is part of the batch requirement.
Discharge design also deserves close attention. A poorly selected valve can retain material from the previous batch, creating cross-contamination or carryover. Slow, non-uniform discharge may allow a blend to separate as it leaves the vessel. For many applications, a full-width bomb-bay discharge provides faster, more complete emptying than a small outlet, reducing residue and supporting more consistent downstream handling.
The right equipment configuration is therefore a process decision, not a catalog decision. PerMix Ribbon Mixers evaluates product characteristics, batch size, sanitation requirements, and processing objectives to help manufacturers select a tailored solution rather than forcing every application into the same mixer design.
Sampling Can Misdiagnose the Process
A batch may be consistent while the sample is not representative. This is particularly common when personnel collect a single grab sample from the top of a container, the beginning of discharge, or one location in a tote. Sampling error can lead teams to change a mixing process that was functioning correctly.
A useful validation plan takes samples at defined locations and times, often throughout the discharge stream. It also specifies sample size, handling method, test method, and acceptance criteria. Sampling should reflect the way customers or downstream equipment receive the product, not simply the easiest place for an operator to access material.
When results show variation, separate within-batch variation from batch-to-batch variation. If samples within one batch differ widely, investigate mixer performance, charging, and raw material distribution. If each batch is internally uniform but differs from other batches, examine weighing accuracy, incoming material properties, storage conditions, and recipe execution.
A Practical Way to Reduce Variation
The fastest path to improvement is to establish a baseline rather than adjust multiple settings at once. Record ingredient lot numbers, moisture, particle size where relevant, actual weights, charge order, batch load, agitator speed, mixing time, temperature, discharge duration, and test results. This creates the evidence needed to identify patterns.
From there, change one influential variable at a time and confirm the result with representative samples. A short production trial may reveal that a revised addition sequence is more effective than adding ten minutes of mixing time. In another application, better feeder calibration may solve a problem that appeared to be caused by the mixer.
Preventive maintenance should be part of the same control strategy. Inspect ribbon condition, shaft alignment, bearings, seals, drive components, and discharge mechanisms on a defined schedule. Also verify that cleaning procedures remove retained material without introducing moisture, cleaning chemical residue, or operator-to-operator variation.
Reliable batch consistency comes from treating mixing as a controlled manufacturing operation, not a timed step between weighing and packaging. When material behavior, equipment design, and operating discipline are aligned, manufacturers can reduce rework, protect product quality, and run each batch with greater confidence.