How to Mix Abrasive Powder Safely at Scale
Abrasive powders can damage more than a mixer. Fine silica, alumina, garnet, silicon carbide, metal oxides, and similar materials can create airborne exposure concerns, accelerate equipment wear, and turn a routine batch into a housekeeping or maintenance issue. Knowing how to mix abrasive powder safely means controlling the material from receiving through discharge, not simply selecting a mixer with enough capacity.
For plant managers and process engineers, the objective is straightforward: achieve a uniform blend while protecting operators, preserving equipment life, preventing cross-contamination, and maintaining predictable cycle times. The right process depends on particle size, dustiness, hardness, moisture sensitivity, batch volume, and the properties of every ingredient in the formulation.
Start With the Powder Hazard Profile
Abrasive is a functional description, not a complete safety classification. One abrasive powder may be relatively coarse and low-dust, while another may contain respirable fines that require far more stringent exposure controls. Review the current Safety Data Sheet for every material, including minor additives, before defining the mixing procedure.
The hazard review should establish whether the powder presents inhalation, skin, eye, combustible dust, static electricity, or chemical compatibility concerns. Crystalline silica deserves particular attention because respirable exposure can create serious long-term health risks. Do not assume that a mineral powder is nonhazardous because it is inert in the finished product.
Particle size distribution matters as much as chemistry. Fine particles generally become airborne more easily, can adhere to surfaces and seals, and may be more difficult to discharge completely. Coarser abrasive media may produce less dust but can increase mechanical wear on ribbons, troughs, valves, and downstream conveying equipment.
Engineer Dust Control Before Charging the Mixer
The safest powder is the powder that stays contained. Open-top charging methods can expose operators even when they wear appropriate personal protective equipment. Whenever practical, use enclosed transfer from bags, drums, bulk bags, hoppers, or pneumatic conveying systems into a sealed mixer inlet.
Local exhaust ventilation should capture dust at the point where it is generated, particularly at bag dumping stations, charging ports, sampling points, and discharge connections. The system must be designed for the powder’s characteristics and verified through regular inspection. A dust collector that is undersized, poorly maintained, or positioned too far from the source will not deliver reliable protection.
Where combustible dust is possible, the process requires a documented dust hazard analysis and equipment designed for the applicable hazard classification. This may involve grounding and bonding, ignition source control, explosion venting or suppression, isolation devices, and appropriately rated electrical components. The correct safeguards depend on the material test data and the full process layout, not on a generic assumption about powder handling.
Housekeeping supports containment. Accumulated dust can be disturbed by foot traffic, vibration, or maintenance activity. Use approved industrial vacuum systems suited to the material hazard. Avoid dry sweeping and avoid blowing powder from equipment with compressed air, which can create an exposure cloud and spread contamination through the production area.
Use PPE as the Final Layer of Protection
Personal protective equipment is necessary, but it should not be the only control. When enclosure and ventilation are working correctly, PPE provides an additional barrier against residual exposure during charging, sampling, cleaning, and maintenance.
The required PPE should follow the SDS, site risk assessment, and applicable regulatory requirements. Depending on the material, this may include safety glasses or sealed goggles, protective gloves, coveralls, safety footwear, and respiratory protection. If respirators are required, the facility needs a formal respiratory protection program that addresses medical clearance, fit testing, training, cartridge selection, inspection, and replacement schedules.
Operators should also understand why PPE requirements change between activities. A closed, automated batch may involve minimal direct contact, while bag emptying, manual additions, or opening a mixer for cleaning can substantially increase the exposure potential.
How to Mix Abrasive Powder Safely in a Ribbon Mixer
Ribbon mixers can provide efficient, homogeneous blending for many abrasive powder formulations, particularly when the process calls for consistent movement of materials across the full batch. The outer and inner ribbons move material in opposing directions, helping reduce localized concentration differences when the mixer is properly sized and operated.
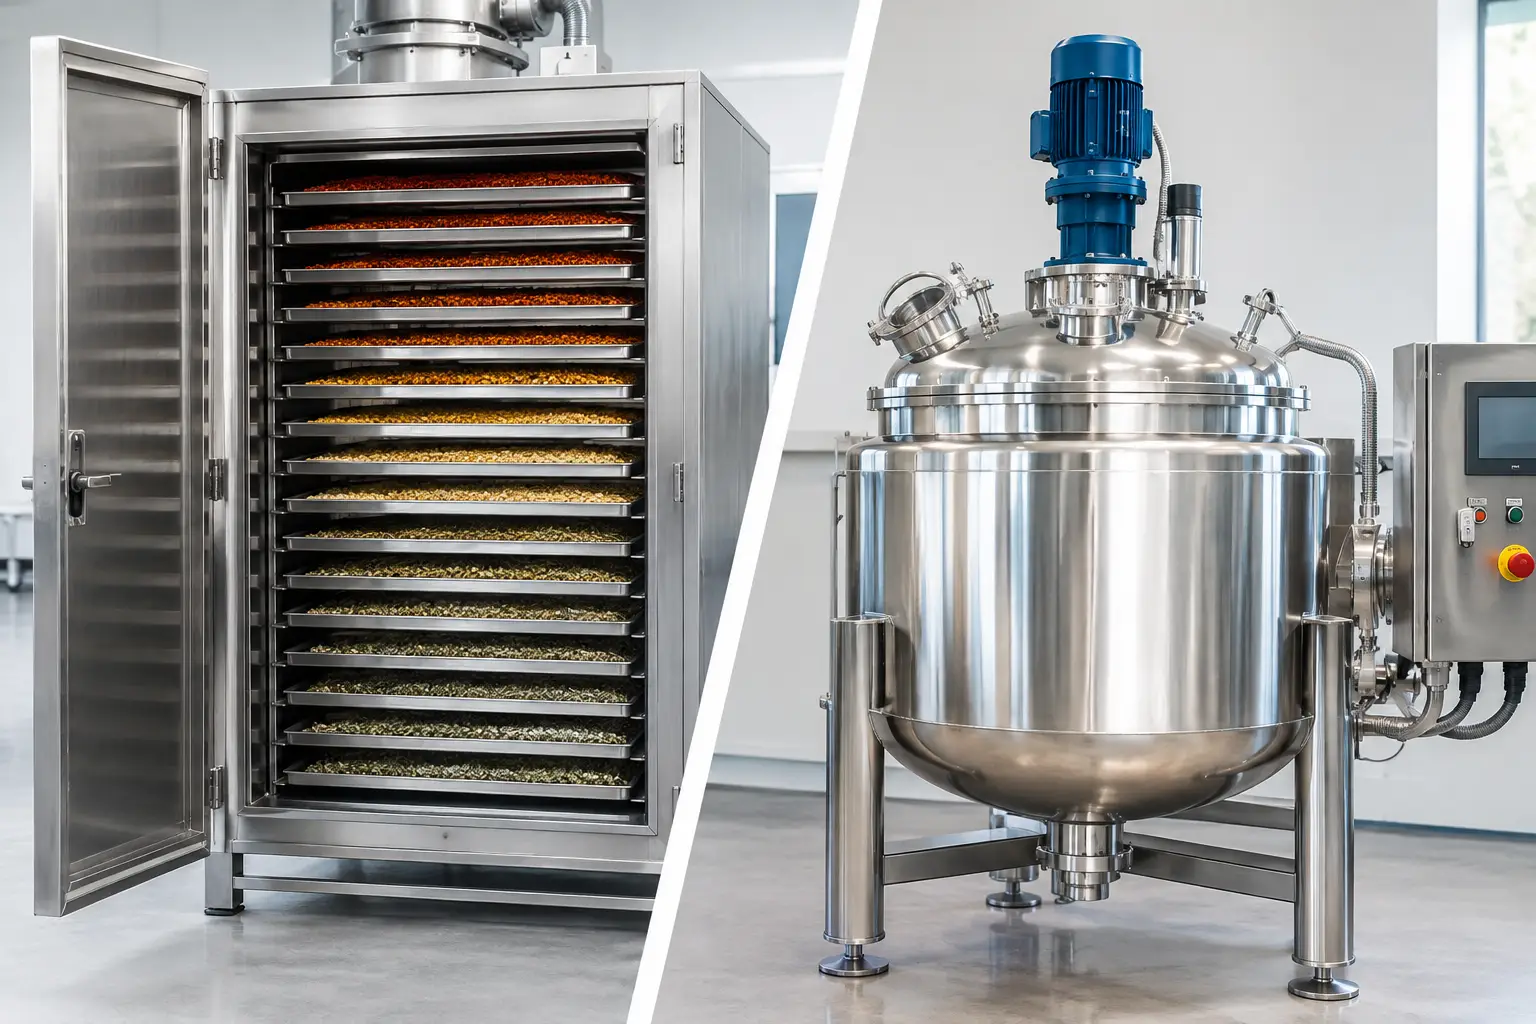
However, abrasive service must be addressed during equipment selection. Material hardness, bulk density, particle morphology, and batch frequency all affect wear rates. A mixer built for light food powders may not be appropriate for dense mineral blends or high-throughput abrasive compounds. Engineering decisions may include wear-resistant contact surfaces, heavy-duty ribbons, reinforced discharge valves, upgraded shaft sealing, and drive components matched to the required torque.
Do not overfill the mixer. A ribbon mixer needs adequate free volume for the material to circulate. Underfilling can also reduce mixing efficiency, especially when low-volume ingredients must distribute through a large batch. The practical operating range depends on the mixer geometry, formulation behavior, and validated batch size.
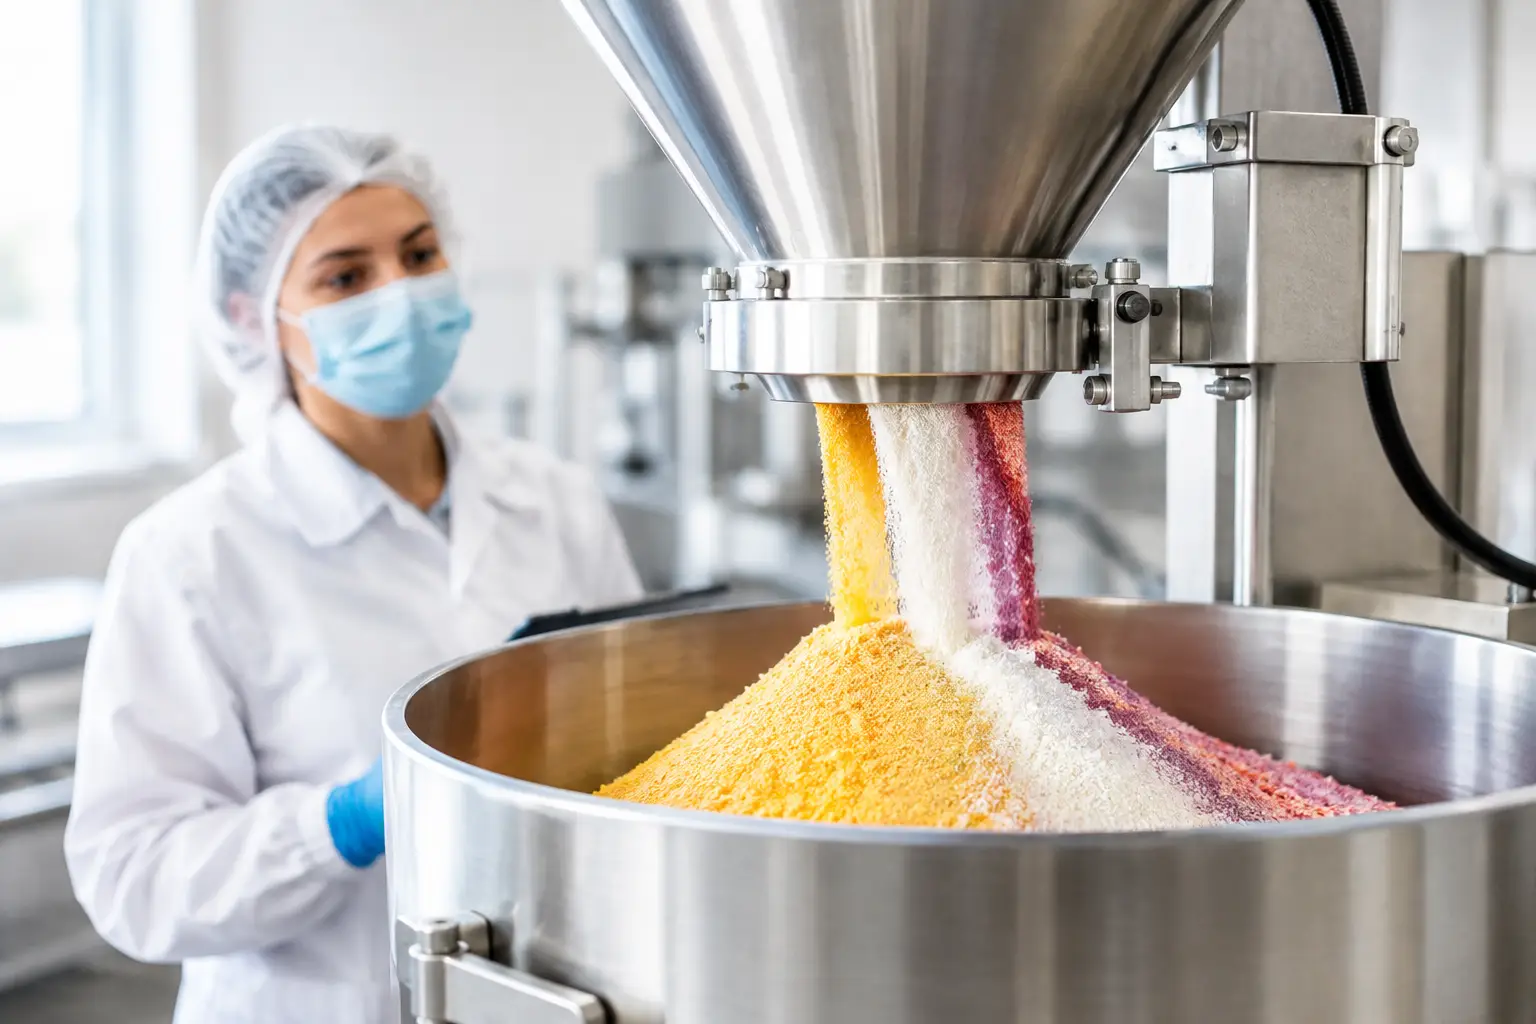
Charging order is equally important. In many applications, larger-volume base powders are loaded first, followed by smaller additions distributed across the batch rather than dumped into one location. If liquids, binders, pigments, or performance additives are present, their introduction rate and location should be controlled to avoid agglomeration. The best sequence should be established through trials and then documented in the batch procedure.
Mix time should be validated, not guessed. Running longer than necessary can waste energy, increase wear, and in some cases promote particle attrition or segregation. Running too briefly creates a nonuniform product. Representative sampling from multiple locations and repeatable quality testing are the practical way to establish the correct cycle time.
Prevent Wear, Contamination, and Unplanned Downtime
Abrasive materials place predictable stress on the equipment, but planned maintenance can prevent that stress from becoming an unplanned outage. Inspect ribbons, trough linings, seals, bearings, discharge valves, and shaft interfaces on a schedule based on the material and operating hours. Monitor motor load and batch cycle trends as well. A gradual rise in amperage or a longer discharge time can indicate material buildup, mechanical drag, or developing wear.
Seal selection deserves close attention. Abrasive fines can migrate into unsuitable sealing arrangements and shorten service life. The appropriate design may involve specialized packing, air purges, mechanical seals, or other engineered solutions based on the process pressure, material behavior, and cleaning requirements.
Cross-contamination control is another operational concern. Abrasive residues can remain in corners, discharge zones, and valve seats. For regulated or high-purity production, the mixer should be designed for access, inspectability, and validated cleaning. The cleaning method must control dust and protect surfaces without introducing moisture or incompatible cleaning agents into the process.
Build a Repeatable Batch Procedure
Safe abrasive mixing is most reliable when operators do not have to improvise. A documented standard operating procedure should specify the approved materials, charging sequence, mixer fill level, speed, mix time, dust collection requirements, PPE, sampling plan, discharge method, and cleaning steps.
The procedure should also identify stop-work conditions. These may include a failed dust collector alarm, visible dust escaping from a connection, abnormal mixer vibration, damaged grounding equipment, a seal leak, or an unexpected change in material appearance. Clear escalation steps allow an operator to stop a batch before a small deviation becomes a quality, maintenance, or safety event.
Training should be practical and equipment-specific. Operators need to know how to recognize poor containment, verify that safeguards are functioning, and perform routine inspections without exposing themselves to dust. Maintenance teams need lockout/tagout procedures before accessing internal mixer components or clearing a blockage.
Match the Mixer to the Actual Application
The best equipment choice depends on more than a material name. A process handling fine alumina with a small liquid addition may require a different mixer configuration than one blending coarse silicon carbide with polymer resin or mineral fillers. Batch size, required uniformity, product fragility, discharge needs, sanitation expectations, and wear resistance all influence the final design.
PerMix works with manufacturers to evaluate these process variables and configure ribbon mixing systems around the material, not a generic specification. That approach supports superior mixing performance while helping facilities reduce maintenance exposure, material loss, and avoidable downtime.
A safe abrasive mixing process is built through disciplined material assessment, effective containment, validated operating parameters, and equipment engineered for the duty. When those elements are designed together, operators can run consistent batches with greater confidence and plants can protect both product quality and long-term production capacity.