Pharmaceutical Mixer Containment Guide for Safety
Fine pharmaceutical powders do not need much headroom to become an exposure, housekeeping, or cross-contamination problem. A properly engineered pharmaceutical mixer containment guide starts with the actual material behavior at charging, blending, sampling, and discharge – not with a generic enclosure added after installation.
For pharmaceutical manufacturers, containment is a process requirement tied directly to operator protection, product quality, cleaning validation, and batch reliability. The right mixer configuration controls airborne dust while preserving the access, cleanability, and blending performance required for efficient production.
Define the Containment Requirement Before Selecting a Mixer
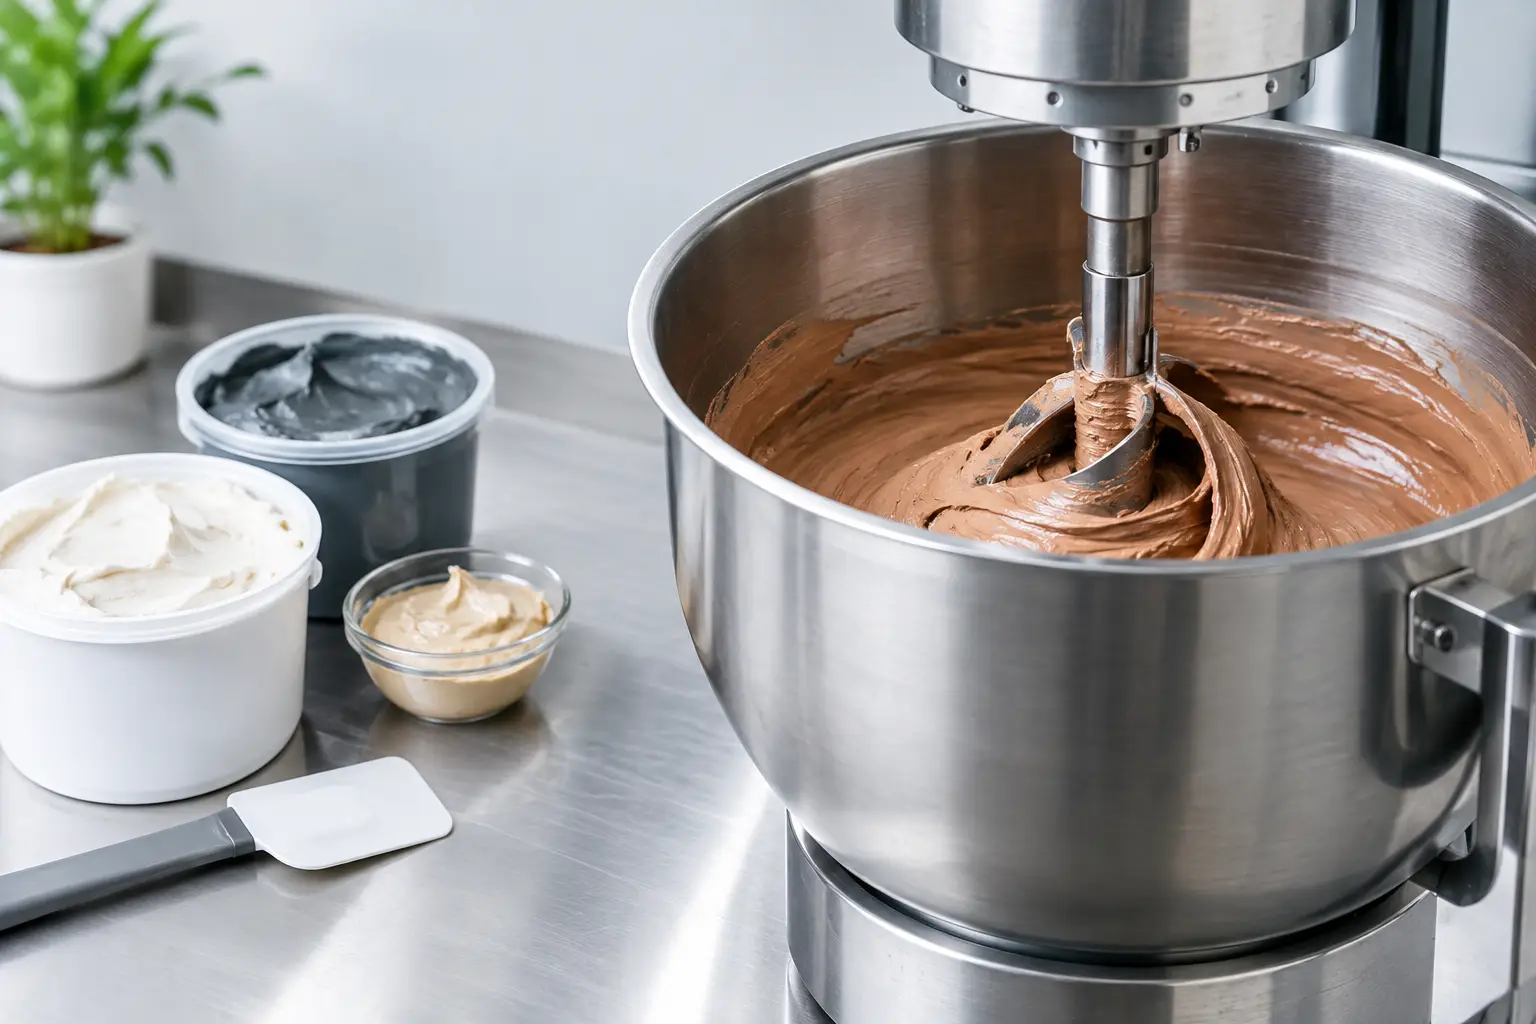
Containment requirements should be established before mixer geometry, capacity, and accessory options are finalized. A ribbon mixer can deliver efficient, homogeneous blending for powders, granules, and paste-like materials, but the containment design must reflect the potency, dustiness, and handling steps of the specific formulation.
Begin with the occupational exposure band or internal exposure limit for the active ingredient and the finished blend. Lower exposure limits generally demand more controlled charging and discharge arrangements, fewer open handling steps, and more stringent verification of seals and interfaces. Material properties matter as well. A free-flowing powder may move quickly through a transfer connection, while a cohesive or electrostatic powder can cling to surfaces, accumulate around gaskets, and release unexpectedly during cleaning or maintenance.
The formulation’s sensitivity to contamination also changes the design decision. A non-sterile dietary supplement premix and a potent pharmaceutical intermediate may both require dust control, but their containment targets, cleaning procedures, and validation expectations are not the same. Treating them as identical applications can create either unnecessary capital cost or inadequate protection.
Where Pharmaceutical Mixing Creates Exposure Risk
The mixing cycle has several potential release points. Containment planning should address all of them rather than focusing only on the mixer vessel.
Charging is often the highest-risk step. Opening a manway, cutting bags, pouring drums, or loading sacks through an uncovered inlet can generate a visible dust cloud and expose personnel before mixing begins. Closed transfer from an intermediate bulk container, vacuum conveying system, or contained bag-dumping station reduces this risk significantly. The best method depends on batch size, flow characteristics, cleaning frequency, and the number of ingredients being introduced.
During mixing, the main concern is leakage through access doors, shaft seals, instrument ports, and vent connections. A horizontal ribbon mixer should maintain a controlled, sealed processing environment while operating. Properly selected gasket materials, precision-fitted covers, and dependable shaft sealing help prevent powder escape without compromising maintainability.
Sampling can also defeat an otherwise well-contained process. If operators must open a cover and insert a thief sampler, the process becomes dependent on procedural controls and personal protective equipment. A contained sampling port or closed sampling method can lower exposure risk while supporting representative quality-control samples.
Discharge deserves equal attention. Product may bridge above the outlet, fall unevenly into a container, or produce a dust plume as air is displaced. A sealed discharge valve and a compatible downstream receiving interface keep the material path controlled. For high-containment applications, the discharge arrangement may require split butterfly valves, continuous liner systems, or another validated contained-transfer approach.
Mixer Design Features That Support Containment
A containment-capable mixer is not simply a standard vessel with more clamps. It is a coordinated equipment design that balances sealing performance, sanitary construction, process access, and reliable material movement.
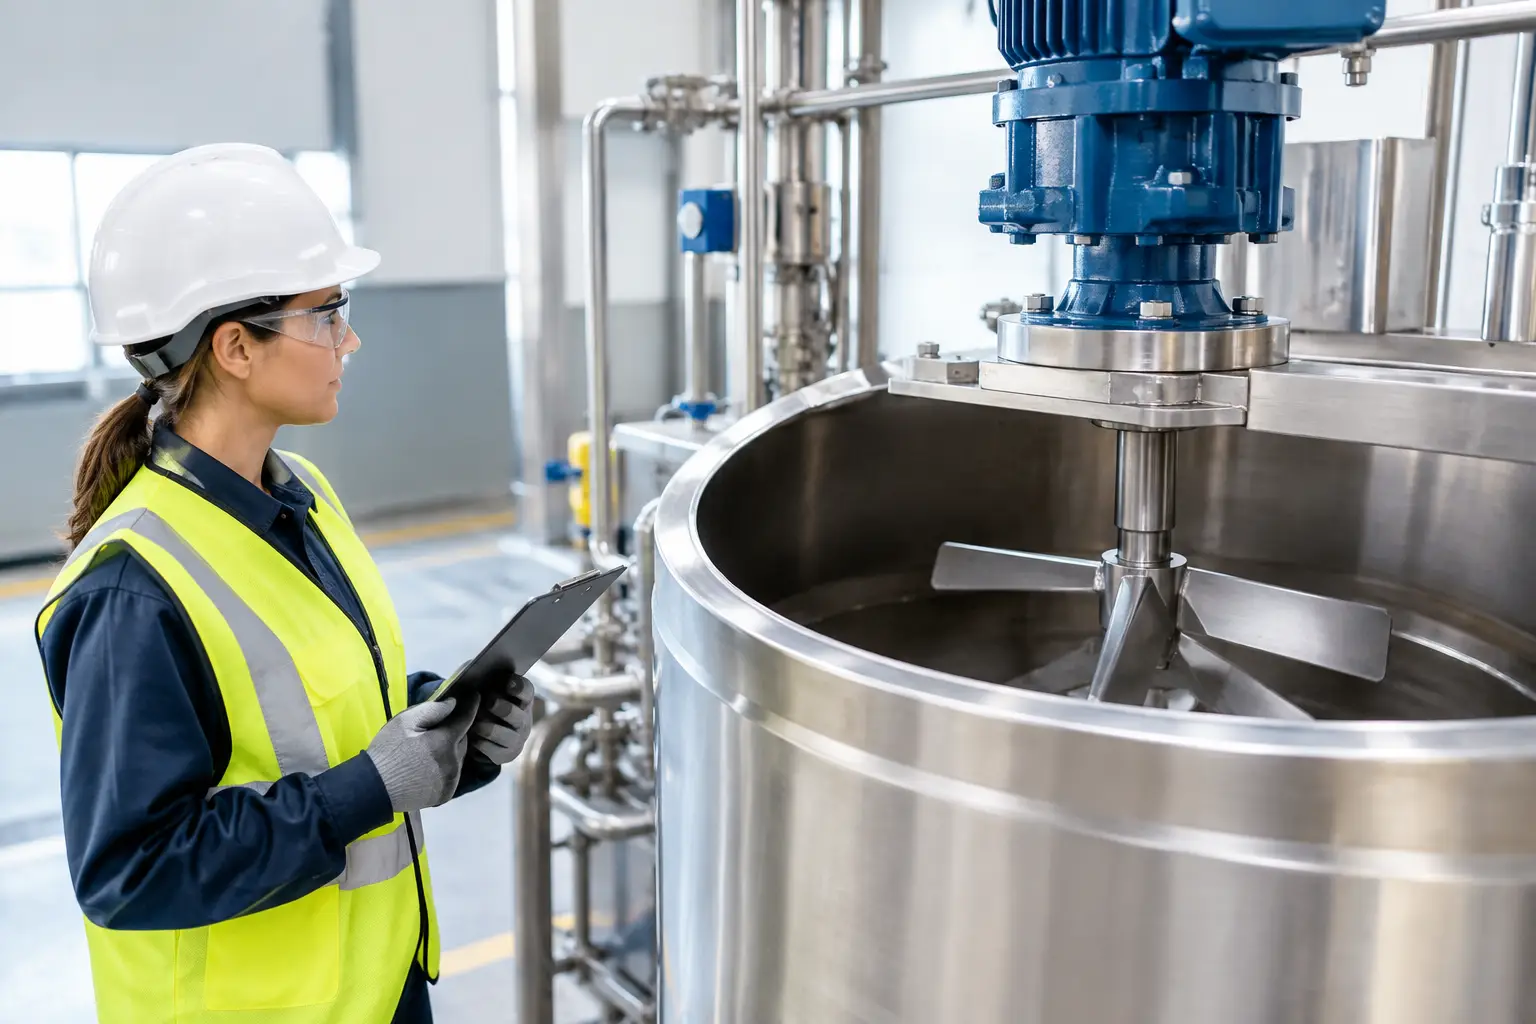
A fully enclosed trough with a fitted top cover provides the basic process boundary. Covers should include only the ports needed for charging, venting, inspection, sampling, or liquid addition. Each unnecessary opening introduces another seal, cleaning location, and potential leak path.
Shaft seals are particularly important because the agitator must rotate while maintaining the integrity of the vessel boundary. The correct seal arrangement depends on operating pressure, powder abrasiveness, required cleaning method, and containment target. In some applications, a standard sanitary packing or mechanical seal may be appropriate. Higher-risk compounds may justify upgraded seal systems, leak detection, or inert gas purge arrangements. The right answer is application-specific, not a single standard feature.
The discharge valve must match both the material and the containment strategy. Butterfly valves can offer compact, efficient control for free-flowing products, while other valve types may be better suited to cohesive materials or applications requiring tighter shutoff. The outlet should be sized to promote complete discharge and minimize residual product. Less retained material means less manual intervention during changeover.
For formulations requiring low moisture exposure, solvent handling, or oxygen control, a vacuum ribbon mixer or dryer can provide an enclosed environment while supporting mixing, drying, and related processing steps in one vessel. This can reduce transfer points, which often improves both containment and operating efficiency.
Sanitary Design and Cleanability Cannot Be Secondary
Containment and sanitation are closely connected. A mixer that contains dust but traps residue in inaccessible areas can create a different compliance problem during cleaning and product changeover.
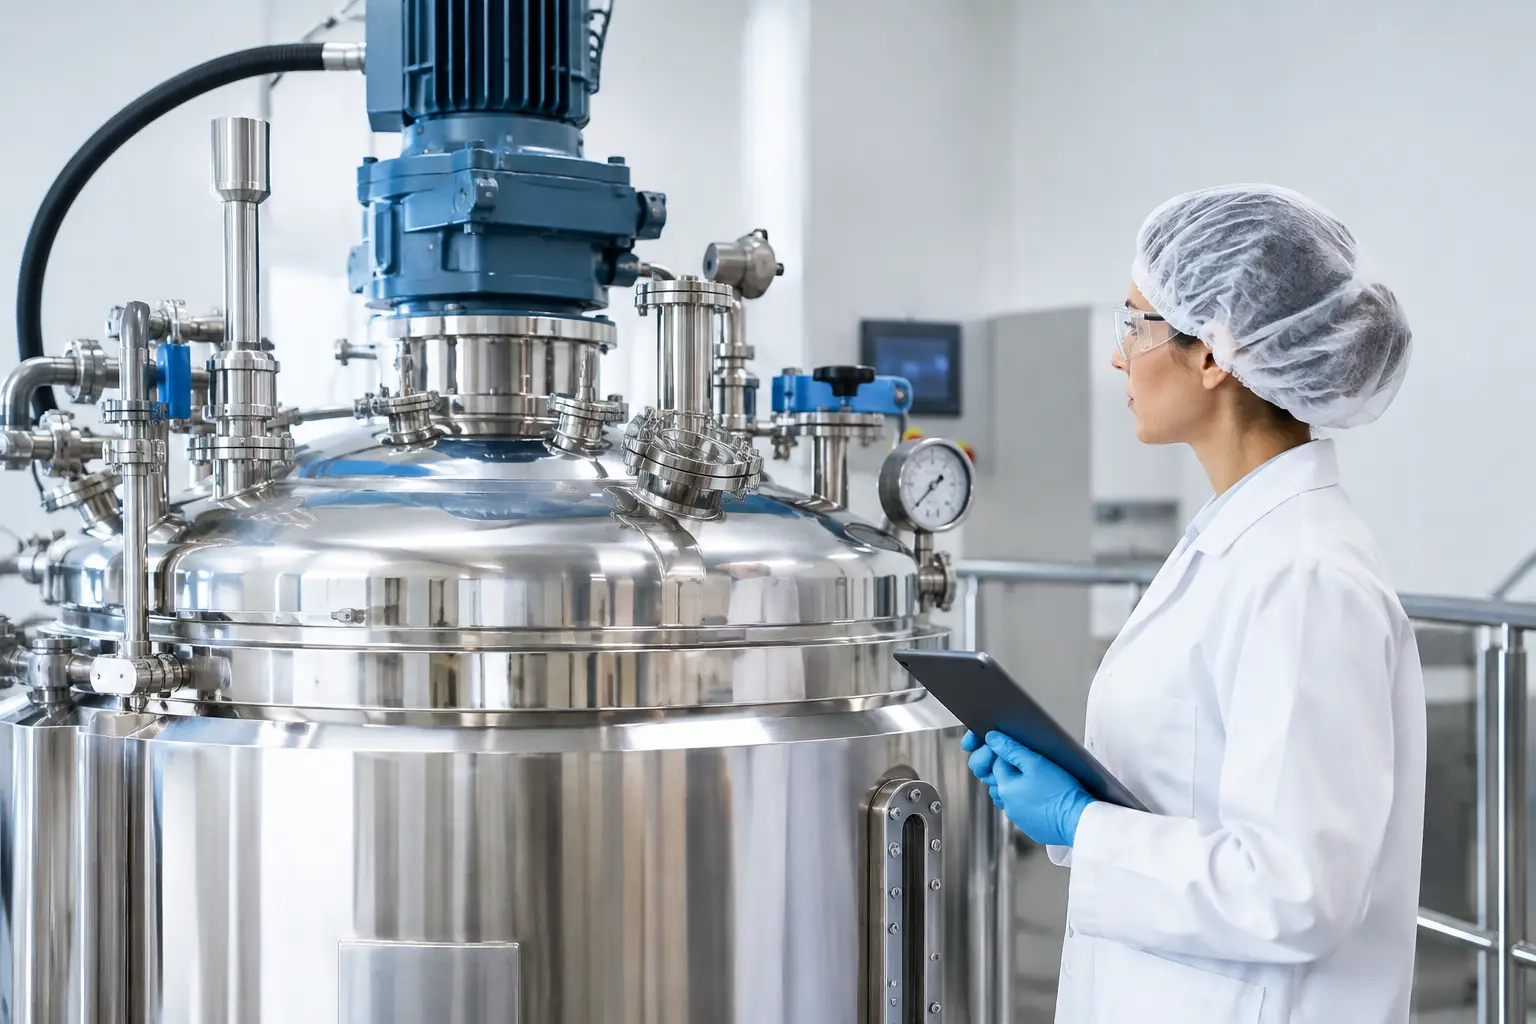
Pharmaceutical mixer contact surfaces should be specified for the required hygienic standard, commonly with polished stainless-steel construction and welds finished to support cleaning. Internal geometry should avoid unnecessary ledges, dead zones, and crevices where material can collect. Ribbon design, agitator clearances, end-wall construction, and discharge configuration all influence how completely a batch can be discharged and how easily remaining residue can be removed.
Cleaning method should be defined early. Manual dry cleaning may be practical for a dedicated-product operation, but it requires safe access and an effective containment procedure for removed powder. Wet cleaning or clean-in-place systems can reduce manual exposure, although they add utilities, validation work, drying requirements, and potential downtime. There is no universal best option. The cleaning approach should match the formulation, campaign length, product-change frequency, and validation strategy.
Build Containment Around the Full Material Path
A mixer is only one component in the containment chain. A highly sealed vessel will not solve exposure problems created by open bag dumping upstream or an uncovered bin downstream.
Evaluate the full material path from receiving through final discharge. This includes raw-material containers, charging equipment, transfer lines, dust collection, sampling devices, and receiving vessels. Equipment interfaces should be mechanically compatible and operationally realistic. For example, a contained inlet is of limited value if operators must disconnect an unprotected flexible hose covered with residual powder after each batch.
Ventilation must also be considered carefully. Local exhaust can capture fugitive dust around non-contained activities, but excessive negative pressure at the mixer can affect powder movement or draw contaminants through poor seals. A properly designed vent filter or dust collection connection helps manage displaced air during charging and discharge without turning the mixer into an uncontrolled air path.
Verify Performance Under Real Operating Conditions
Containment performance should be tested under the conditions the plant will actually use. Verify the equipment during charging, mixing, discharge, cleaning, and routine maintenance, including credible upset conditions such as a blocked filter, partially closed valve, or a difficult-flowing formulation.
A practical verification plan may include visual dust observations, pressure or airflow checks, surface monitoring, and industrial hygiene sampling where required. Operators should be included in the evaluation. They often identify access issues, awkward connections, and cleaning steps that are not obvious on a process flow diagram.
Questions to Ask When Specifying a Pharmaceutical Ribbon Mixer
A useful equipment specification connects process needs to measurable design requirements. Procurement teams and process engineers should establish answers to these questions before requesting a final mixer quotation:
- What is the material’s exposure limit, dustiness, particle size, bulk density, and flow behavior?
- How will ingredients enter the mixer, and can charging remain closed throughout the batch?
- What level of containment is required at discharge, sampling, cleaning, and maintenance?
- Which contact materials, surface finish, gasket compounds, and documentation are needed for the application?
- Will the mixer be dedicated to one product, or must it support validated changeovers?
- Does the batch require vacuum, heating, cooling, liquid addition, or inerting in addition to blending?
These details allow the mixer supplier to recommend a configuration that supports both mixing quality and containment performance. They also reduce the risk of expensive modifications after factory acceptance testing or site installation.
Containment Should Improve Production, Not Slow It Down
The strongest containment strategy protects people without creating an impractical process. Excessively complex connections, difficult-to-clean hardware, or poorly chosen valves can add time to every batch and encourage workarounds on the production floor. Conversely, a well-matched enclosed ribbon mixer can reduce airborne dust, simplify housekeeping, shorten changeovers, and support repeatable batch handling.
PerMix works with pharmaceutical processors to configure ribbon mixing systems around material characteristics, production goals, and sanitary requirements. When containment is considered at the same time as blend uniformity and discharge performance, the resulting equipment is better positioned to protect the operator and keep the process moving.