Ribbon Blender Discharge Problems and Fixes
A ribbon mixer can produce a highly uniform batch and still create a production bottleneck at the point of discharge. Ribbon blender discharge problems often appear as slow emptying, retained material, inconsistent downstream feed, valve leakage, or product separation after mixing. For plant teams handling powders, granules, pastes, and blended formulations, these issues affect more than cycle time. They can compromise yield, sanitation, batch traceability, and product consistency.
Discharge performance is not determined by the outlet alone. It is the result of how the product behaves, how the mixer is configured, how the valve is designed, and how the equipment connects to the next processing step. The most effective solution begins with identifying the true source of the restriction rather than treating every issue as a valve problem.
Why Ribbon Blender Discharge Problems Occur
A horizontal ribbon blender is designed to move material in opposing directions to create a homogeneous blend. Once mixing is complete, that same product must flow efficiently through the discharge opening without excessive manual intervention or residual hold-up. This becomes difficult when the material has poor flow properties, contains cohesive fines, changes behavior with moisture or temperature, or is being discharged into equipment that cannot accept product at the same rate.
The discharge port must also match the process objective. A small outlet may provide controlled feeding, but it can extend emptying time and increase retained product. A larger outlet can improve batch release, but may require a more capable downstream hopper, conveyor, mill, or packaging system. There is no universal outlet size or valve style that works equally well for every product.
Material Bridging and Arching
Bridging occurs when powder or granular material forms a stable arch above the discharge opening. The product remains in the trough even though the valve is fully open. Cohesive materials, fine powders, hygroscopic ingredients, products with broad particle-size distributions, and formulations containing fat or liquid binders are common candidates for this behavior.
A larger discharge opening can help, but size alone is not always the answer. The outlet geometry, internal surface finish, product moisture level, and angle of material flow all matter. In some applications, a full-width or flush-bottom discharge design provides a more reliable release than a conventional center outlet.
Product Retention in the Trough
Residual material left behind after discharge is a direct yield loss. It also creates a serious concern when changing formulas, colors, allergens, active ingredients, or regulated products. Product can collect around valve seats, beneath shaft areas, in transitions, and along trough corners where flow is limited.
Retention may be caused by sticky product, inadequate internal clearances, an outlet that is too small, or insufficient discharge time. It may also indicate that the ribbon arrangement is optimized for mixing but not for sweeping material toward the outlet. For applications requiring low residuals, the mixer configuration should be evaluated as a complete system rather than adjusted after installation.
Valve Selection Does Not Match the Product
Discharge valves are often selected based on availability or initial cost, but their operating characteristics vary substantially. A slide gate may suit free-flowing dry powders. A butterfly valve can be compact and effective in many installations, but may not provide the needed cleanability or flow path for every formulation. Bomb-bay doors, flush valves, and specialized sanitary discharge arrangements can support faster release and lower product hold-up when properly engineered.
The right choice depends on whether the priority is metered discharge, rapid batch dumping, hygienic access, pressure or vacuum integrity, or tight shutoff. Vacuum ribbon mixers and dryers require particular attention because the discharge assembly must maintain process integrity while accommodating the product’s condition at the end of the cycle.
A Practical Way to Diagnose the Discharge Point
Before modifying equipment, observe a complete batch discharge under normal operating conditions. A useful evaluation includes the product condition at the end of mixing, actual time to empty, residual material quantity, valve operation, and behavior of the downstream equipment. This often reveals whether the restriction is inside the mixer or below it.
Four observations are especially valuable during troubleshooting:
- Does material stop flowing while a significant volume remains in the trough?
- Does the discharge rate surge, pulse, or remain consistently slow?
- Is product accumulating at the valve, chute, or receiving hopper?
- Does the problem occur with every batch or only with certain formulations, temperatures, or fill levels?
If flow stops above the outlet, bridging or poor product flowability is likely. If the product exits the mixer but backs up immediately below the valve, the downstream process is limiting throughput. If residual material is concentrated around the valve, the discharge geometry or valve seat may need attention. A problem limited to certain batches may point to changes in raw-material moisture, particle size, liquid addition, or blend temperature.
Correcting Slow or Incomplete Discharge
The corrective action should address the process requirement, not simply force product through an undersized opening. For example, vibration may break a bridge in a dry powder, but it can cause segregation in a blend containing particles of different sizes or densities. Mechanical agitation near the outlet may improve release for one product while damaging fragile granules in another.
Match Outlet Size to Product Flow
For materials that discharge slowly despite being reasonably free-flowing, increasing the outlet area may be the most direct improvement. A larger discharge opening reduces the likelihood of stable bridges and lowers the time required to empty the trough. However, it must be coordinated with the receiving equipment. An oversized outlet that overwhelms a screw feeder or packaging line simply moves the bottleneck downstream.
For controlled feeding, a smaller outlet combined with an appropriate feeder may be preferable. This is common when a ribbon blender feeds extrusion, tableting, filling, or other processes that require a consistent material rate. The design objective is not always the fastest discharge. It is dependable, repeatable discharge at the rate the overall line can use.
Specify the Right Valve and Actuation
Valve performance should be evaluated for sealing, cleanability, opening area, product contact surfaces, and control method. Pneumatic actuation is common in automated production because it provides repeatable opening and closing. Yet the actuator must have sufficient force to operate reliably if product compacts around the valve or if the process handles sticky materials.
For sanitary or high-purity applications, valve accessibility is equally important. Operators need a practical way to inspect, clean, and verify the discharge zone. A valve that is difficult to access can turn a minor residual issue into prolonged downtime during changeover.
Improve Product Condition Before Discharge
Some discharge problems begin upstream. Excessive liquid addition, poor raw-material storage, high humidity, and temperature changes can convert a free-flowing blend into a cohesive mass. Testing bulk density, moisture content, particle size, and angle of repose provides a more reliable design basis than assuming a product will behave like a similar-looking powder.
This is especially relevant for products that change during mixing. A powder may become less flowable after liquid is introduced, while a heated formulation may become more viscous as it cools. When batch conditions vary, the discharge system needs enough operating margin to handle the most demanding realistic case, not only the ideal one.
Preventing Segregation During Emptying
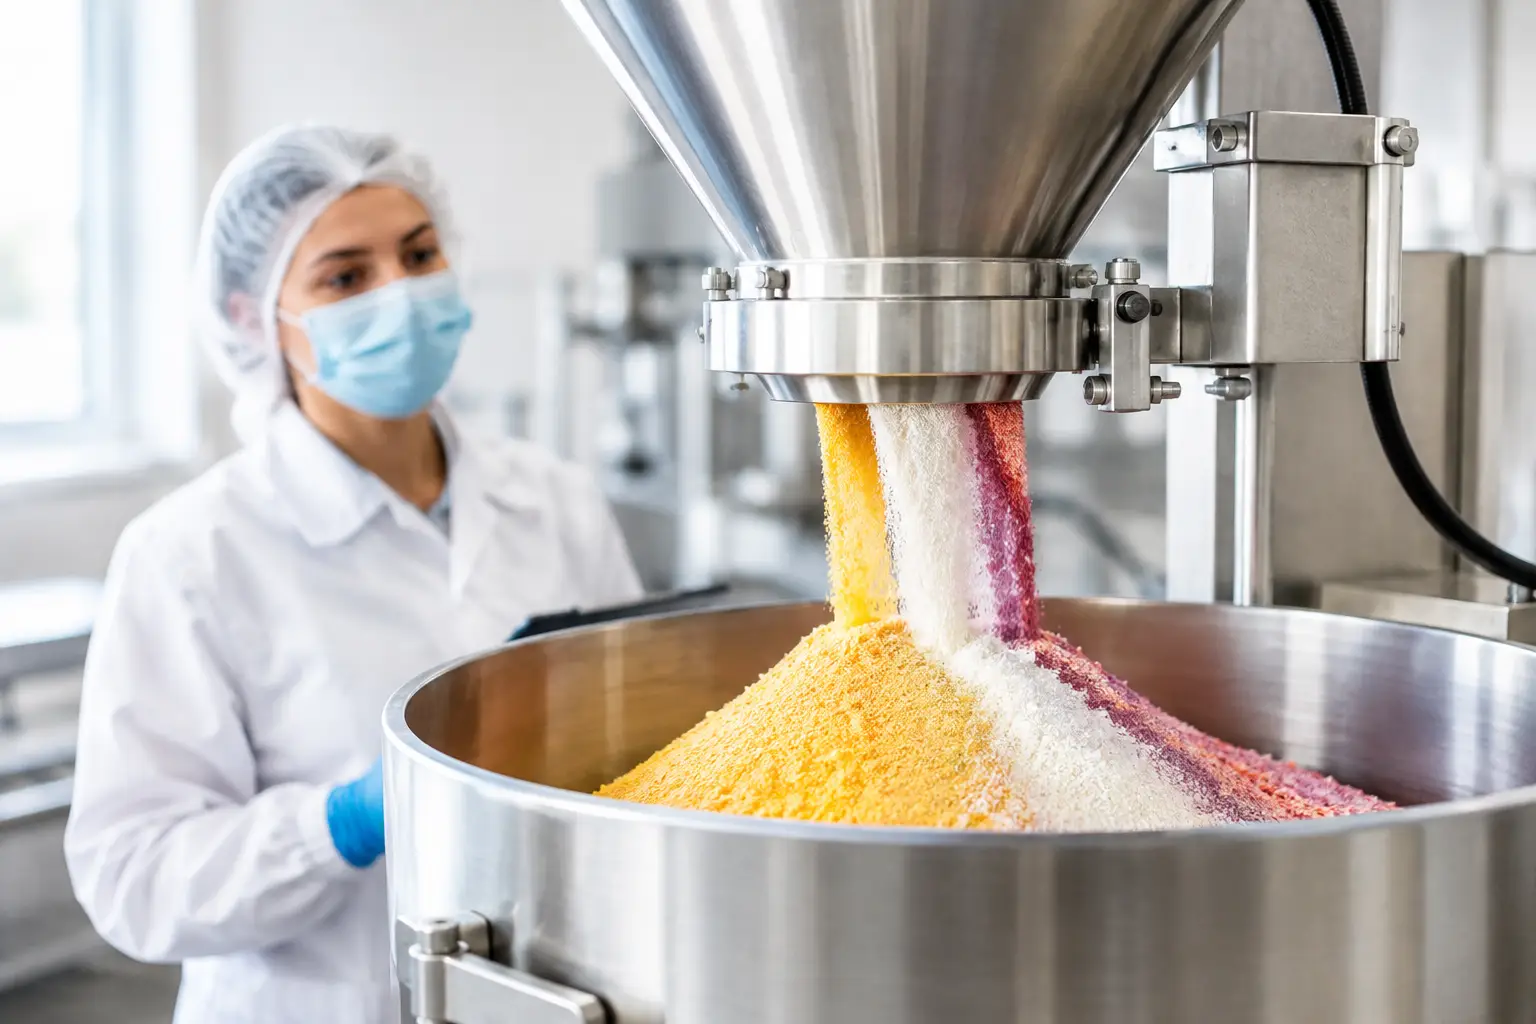
Fast discharge is valuable, but it should not come at the expense of blend uniformity. Segregation can occur when a mixed product drops through a long vertical chute, experiences high impact, or feeds unevenly into a receiving vessel. Differences in particle size, density, and shape increase the risk.
A properly designed discharge transition minimizes uncontrolled free fall and avoids ledges where fine material can collect. Where practical, the receiving equipment should be positioned close to the mixer outlet and designed to accept the product without creating a new separation point. For fragile or segregating products, controlled discharge may be more valuable than maximum dump speed.
Design Decisions That Reduce Downtime
The best time to solve discharge issues is during equipment specification. Process engineers should provide representative material data and explain the complete process sequence, including batch size, desired emptying time, downstream equipment, cleaning method, and any sanitary or containment requirements. A mixer should be designed around how the product is actually produced, not only how it mixes in a laboratory sample.
Configuration options such as trough shape, discharge location, valve type, internal finish, access doors, and automation controls can materially affect daily operation. PerMix applies application-specific engineering to help customers balance mixing quality, discharge efficiency, cleanability, and long-term maintenance requirements.
For existing equipment, a focused review can often identify practical upgrades without replacing the entire mixer. That may include modifying the discharge valve, improving the transition below the outlet, adjusting operating procedures, or evaluating whether product conditioning has changed since the mixer was installed.
A discharge system earns its value when operators can empty each batch predictably, clean it efficiently, and feed the next process without intervention. Treating the outlet as part of the mixing process, rather than a simple exit point, gives plant teams a clearer path to higher yield and more dependable production.