How to Select Vacuum Drying Mixers for Production
A vacuum drying mixer can solve two costly process problems in one vessel: uneven product blending and slow, energy-intensive moisture removal. But the wrong configuration can create new constraints, from poor material turnover and extended cycle times to difficult cleaning and inconsistent final moisture. Knowing how to select vacuum drying mixers begins with the material, then moves through drying duty, vessel design, utilities, controls, and validation requirements.
For manufacturers processing powders, granules, wet cakes, pastes, or heat-sensitive ingredients, the goal is not simply to purchase a mixer with a vacuum connection. The objective is to specify a system that delivers uniform mixing, predictable drying, practical sanitation, and dependable batch-to-batch performance under real production conditions.
Start With the Material and Process Duty
The material profile determines whether a vacuum ribbon mixer and dryer is appropriate and how it should be configured. A free-flowing powder behaves very differently from a cohesive filter cake, a viscous paste, or a blend that becomes sticky as liquid is removed. The product’s condition at the beginning, middle, and end of the cycle all matter.
Document the starting moisture, target residual moisture, batch size, bulk density, particle-size distribution, and angle of repose. Also identify whether the material is hygroscopic, abrasive, corrosive, heat-sensitive, solvent-bearing, or prone to agglomeration. These details influence the agitator geometry, heating surface, vacuum level, seal design, construction materials, and discharge arrangement.
A key question is whether the process needs drying and blending at the same time or in separate stages. Vacuum drying mixers are particularly valuable when ingredients must remain homogeneous while moisture or solvent is removed. The agitator continually renews product contact with the heated vessel wall and exposes wet material to the low-pressure environment. This supports more even heat transfer than static vacuum drying, while reducing the risk of localized overheating.
However, not every product benefits from aggressive agitation. Fragile crystals, coated particles, and materials with a narrow acceptable particle-size range may require lower tip speeds and a gentler ribbon configuration. When attrition is a concern, ask for trials that measure particle integrity after a complete drying cycle, not merely after a short mixing test.
Match Mixer Geometry to Product Movement
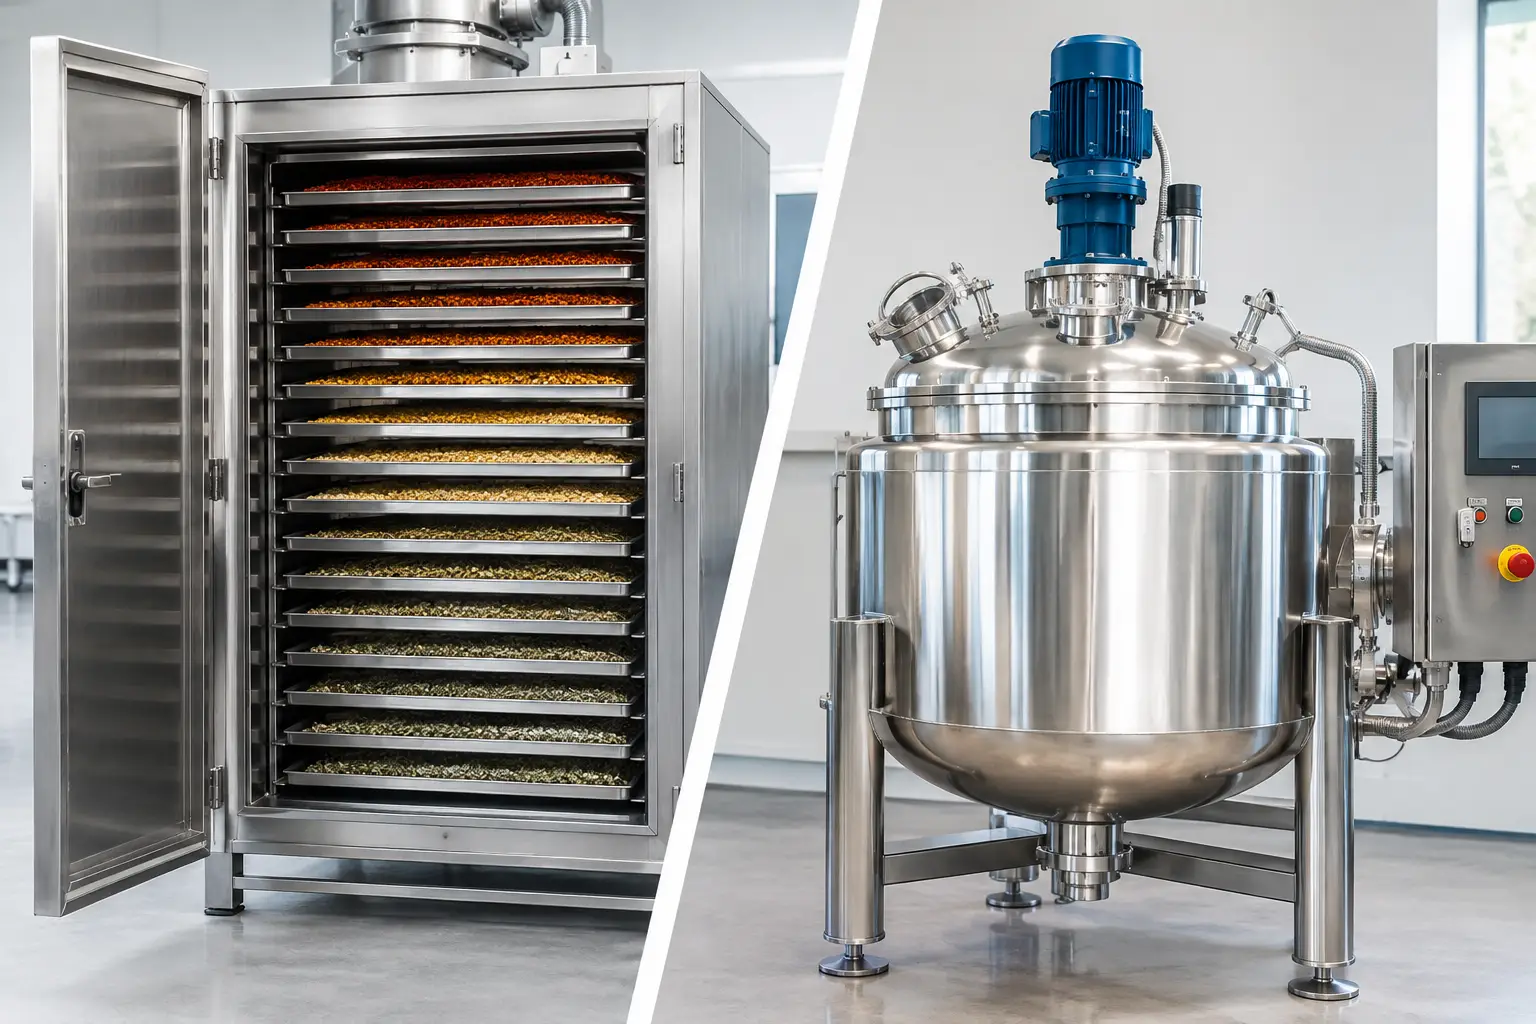
Horizontal ribbon systems are widely used because they provide strong axial and radial movement across the batch. Outer ribbons move material in one direction while inner ribbons move it in the opposite direction, creating a controlled circulation pattern. In vacuum drying service, this movement helps prevent stagnant zones and continually brings fresh product into contact with the heated surfaces.
Mixer geometry should be selected based on fill level, product flow behavior, and discharge needs. Many processes perform best within a defined working volume rather than at the vessel’s maximum nominal capacity. Underfilling can reduce effective ribbon engagement, while overfilling can restrict circulation and compromise vapor release from the product bed.
For cohesive, sticky, or paste-like materials, a standard ribbon arrangement may need support from additional design features. Choppers, intensifiers, or alternative agitator elements can help break down lumps and improve heat exposure. Yet these additions also introduce trade-offs: more mechanical complexity, potentially higher energy consumption, and additional cleaning points. The correct choice depends on whether lump formation is occasional, inherent to the material, or caused by an upstream process issue that should be corrected first.
Discharge is equally important. A mixer that dries effectively but retains product in the vessel can reduce yield and extend changeover time. Evaluate the outlet valve style, discharge location, product bridge tendency, and whether the material will be conveyed directly to downstream screening, packaging, or a reactor. For high-value products, even a small amount of retained material can have a meaningful financial impact.
Define the Drying Target, Not Just the Vacuum Level
Vacuum lowers the boiling point of water and many solvents, allowing drying at reduced product temperatures. That makes it useful for heat-sensitive materials, but vacuum alone does not determine drying performance. Drying rate depends on heat-transfer area, jacket temperature, product movement, vapor path capacity, condenser performance, and the ability to maintain stable operating pressure.
Specify the required final moisture or residual solvent level, the permitted product temperature, and the maximum acceptable cycle time. These targets should be based on measured process requirements, not broad assumptions. A pharmaceutical intermediate may require tightly controlled residual solvent limits, while a food ingredient may prioritize final water activity, powder flow, or protection of flavor compounds.
The heating medium must match the operating temperature range and available plant utilities. Hot water, thermal oil, and steam each offer different performance characteristics. Steam can deliver rapid heat input where suitable utility pressure is available. Thermal oil supports higher-temperature operation and precise control in demanding applications. Hot water may be appropriate for gentler duty and lower temperature requirements.
It is also essential to size the vapor-handling system as a complete package. The vacuum pump, condenser, receiver, piping, and filtration components must manage the expected vapor load without pressure instability. Inadequate condensation capacity can burden the pump, extend drying time, and create unnecessary maintenance exposure. For solvent applications, recovery, emissions control, and compatibility with hazardous vapor service require early engineering review.
Select Construction, Seals, and Finishes for the Environment
Product-contact materials should be selected for corrosion resistance, cleanability, and regulatory fit. Stainless steel is common for food, pharmaceutical, cosmetic, and many chemical applications, but the exact grade depends on the product chemistry, cleaning agents, chloride exposure, and operating temperature. Abrasive products may also require wear protection in high-contact areas.
The shaft seal deserves close attention because it is a critical boundary between the vacuum process and the surrounding environment. Seal selection depends on vacuum level, operating temperature, product characteristics, clean-in-place requirements, and containment expectations. A seal that performs adequately in atmospheric mixing service may not be suitable for sustained vacuum drying duty.
Surface finish requirements should be defined according to the application. Highly sanitary processes may need polished internal surfaces, minimized crevices, clean-in-place spray coverage, and documentation that supports validation. Industrial chemical operations may place greater emphasis on durability, access for inspection, and resistance to aggressive cleaning methods. In either case, avoid specifying a finish by habit. Match it to product risk, cleaning method, and compliance obligations.
Build Safety and Controls Into the Specification
Vacuum drying can involve combustible dusts, flammable solvents, elevated temperatures, and oxygen-sensitive products. The equipment specification should address the actual hazard profile of the process, including dust classification, inerting needs, grounding, pressure relief, temperature monitoring, and explosion-protection requirements where applicable.
For solvent-bearing materials, consider whether nitrogen blanketing is required before, during, or after drying. Oxygen control may protect both product quality and personnel, but it must be integrated with the vessel, vacuum system, condenser, and operating procedures. A poorly coordinated inerting strategy can increase gas consumption without delivering meaningful risk reduction.
Controls should provide operators with usable process information, not just a collection of instrument readings. Batch recipes, temperature ramps, agitator speed control, vacuum setpoints, trend data, and endpoint logic can improve repeatability while reducing operator dependence. Final moisture may be confirmed through laboratory sampling, but process indicators such as pressure behavior, condensate rate, product temperature, and torque can provide valuable evidence that the drying cycle is approaching completion.
Automation needs vary by plant. A development-scale system may benefit from flexible manual control and detailed data capture. A high-throughput production line may require recipe management, electronic batch records, interlocks, and integration with plant control systems. Specify the level of automation that supports your operating model without adding complexity that the team cannot maintain.
Evaluate Cleanability, Maintenance, and Lifecycle Cost
Capital price matters, but a vacuum drying mixer should be evaluated over its operating life. The lowest initial-cost system can become expensive if it has long cleaning cycles, difficult access, frequent seal replacement, excessive utility demand, or limited local service support.
Ask practical maintenance questions during the selection process. Can the agitator, seals, valve, and vacuum components be inspected without major disassembly? Are wear parts standardized and available on a reasonable lead time? Does the design allow safe access for cleaning and servicing? These questions often reveal more about long-term uptime than a specification sheet alone.
Energy performance also deserves attention. Efficient heat transfer, stable vacuum operation, appropriate insulation, and properly sized drives can reduce the cost per batch. The best design is not always the one with the fastest theoretical drying rate. A balanced solution may use less energy, preserve product quality, and provide a more consistent total cycle time.
Use Trials to Confirm How to Select Vacuum Drying Mixers
Process trials are the most reliable way to reduce selection risk, especially for materials with changing rheology, strict moisture limits, or high product value. A useful trial should reproduce the expected starting condition and assess mixing uniformity, drying profile, product temperature, final moisture, discharge behavior, cleanability, and particle condition.
Do not rely only on a vendor demonstration using a surrogate powder. A representative material trial can expose issues such as wall buildup, caking, vapor bottlenecks, or extended drying near the endpoint. Those findings allow the equipment design to be adjusted before fabrication, when changes are more practical and less costly.
A qualified equipment partner should translate trial results into a clear operating window: recommended batch range, agitator speed, heating medium conditions, vacuum target, estimated cycle time, and cleaning approach. PerMix applies this application-specific engineering approach to help manufacturers align vacuum ribbon mixer and dryer configurations with actual production demands.
The most productive purchase decision comes from treating the vacuum drying mixer as part of a complete process, not as a standalone vessel. Bring material data, production targets, utility limitations, safety requirements, and downstream handling needs into the discussion early. That preparation gives your engineering team a stronger basis for selecting equipment that keeps product moving, drying reliably, and production schedules on track.